How Should a Brush Cutter Manufacturer Test a GX35 Wheeled Unit?
See how a brush cutter manufacturer should test a GX35 wheeled unit for cold start, warm idle, throttle response, clutch engagement and shutdown.
Brush Cutter Manufacturer Final Test: GX35 Wheeled Machine Inspection Sequence
A brush cutter manufacturer final test should follow a defined operating sequence, not end after the engine starts successfully. On a GX35 wheeled brush cutter, pre-start preparation, cold starting, warm idle, throttle response, cutting-system engagement, shutdown and post-run inspection reveal different types of production problems.
For importers approving a bulk order, this distinction matters. A completed machine may pass its wheel, frame and engine-mounting checks but still show abnormal throttle return, clutch engagement or vibration during operation. A consistent final test helps separate those problems before shipment without turning routine factory inspection into an unnecessary endurance test.
1. Establish the GX35 Production Reference Before Testing
A final functional test is useful only when the inspector knows which machine configuration is being evaluated. The approved engine, control system, cutting assembly and wheeled structure should form the reference for the inspection.
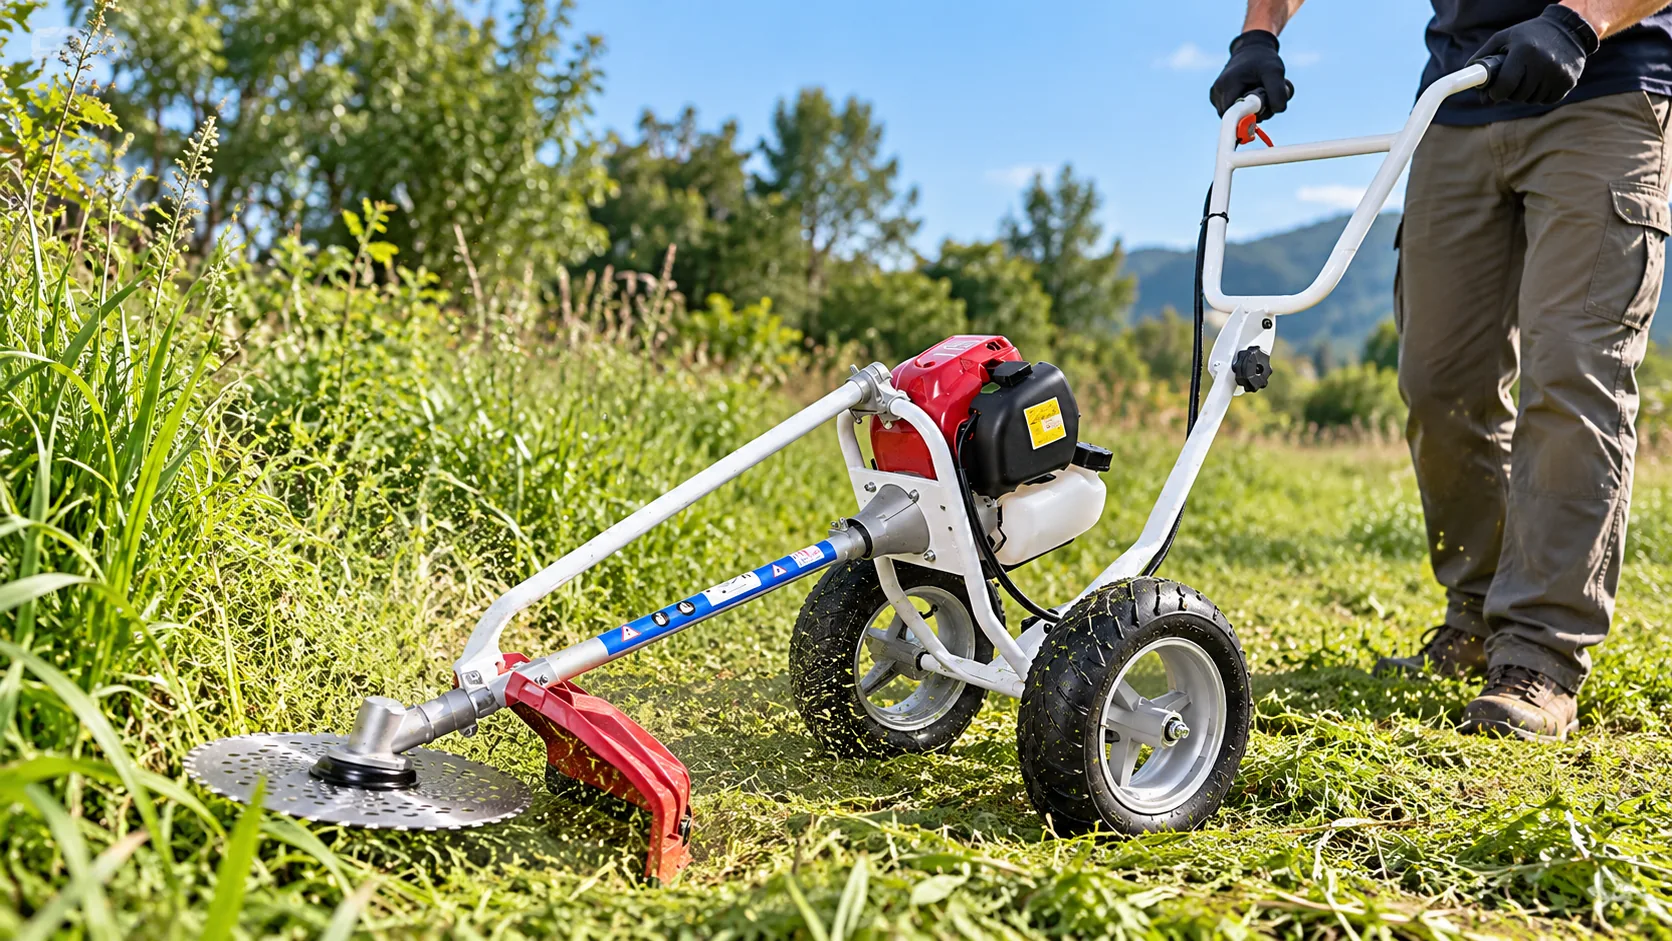
The TM-WBC435 wheeled brush cutter uses a GX35 four-stroke air-cooled engine with 35.8cc displacement and rated output of 1.1 kW at 6500 rpm. Its published specifications also include an idle reference of 3000 ±200 rpm, maximum speed of 10000 rpm, diaphragm carburetor, 800 ml fuel tank and 18.0 kg net weight.
The purpose of the final test
Confirm that the finished TM-WBC435 starts, warms, idles, accelerates, transfers drive and shuts down normally according to its approved configuration. The test is not an attempt to make every published RPM value appear during one short production run.
2. Complete Static Assembly and Four-Stroke Preparation First
A brush cutter manufacturer should not start a finished unit to discover loose mounting hardware or an incorrectly installed cutting assembly. Those problems belong to the static inspection stage and should be corrected before powered operation.
The GX35 engine also requires four-stroke preparation. A two-stroke mixed-fuel procedure must not be applied simply because other brush cutters on the production line use two-stroke engines. Engine-oil grade, quantity and checking method must follow the operating information applicable to the actual engine supplied.
| Inspection Area | Before-Start Requirement | Reason |
| Frame and wheels | Check installed condition, visible alignment and secure assembly. | Prevent structural defects from entering the running test. |
| Engine mounting | Inspect mounting points and visible fasteners. | Avoid confusing loose mounting with engine vibration. |
| Controls | Confirm correct installation and free throttle-return movement. | Identify assembly-related control issues before running. |
| Cutting assembly | Confirm installation matches the approved machine setup. | Reduce risks during cutting-system engagement. |
| GX35 preparation | Verify fuel and engine-oil preparation against confirmed four-stroke instructions. | Avoid invalid test results caused by incorrect preparation. |
Any visible distortion, unsecured component or incorrectly installed cutting-side part should be corrected before starting. Powered testing must take place in a controlled area using the applicable operating and factory safety procedures.
3. Follow the Same Operating Sequence on Every Selected Unit
A repeatable test order makes observations more useful. If inspectors accelerate one machine immediately after startup but allow another to warm first, the differences in operating condition can make the results difficult to compare.
For a finished GX35 wheeled brush cutter, the following sequence separates initial starting, warmed engine behavior, drive engagement and shutdown. The duration and detailed acceptance method should follow the manufacturer's approved test procedure.
STEP 01 — Initial Start
Identify whether the engine is cold or already warm. Follow the applicable starting procedure and observe whether it continues running as the starting controls return to their normal positions. A single ignition event is not enough to establish a successful start.
STEP 02 — Warm Idle
Allow the engine to reach an appropriate operating condition before assessing idle. With the throttle released, observe whether engine speed settles toward the confirmed idle reference without repeated stalling or unexplained high speed.
STEP 03 — Repeated Throttle Response
Increase throttle progressively, release the trigger and observe the return toward idle. Repeat the cycle to identify inconsistent acceleration, sticking controls or abnormal throttle return.
STEP 04 — Cutting-System Engagement
Observe when the cutting system begins receiving drive according to the approved design. Distinguish hesitation before engagement from mechanical noise or vibration that develops only after the cutting system starts operating.
STEP 05 — Stop and Restart Check
Use the designated stop control and confirm normal shutdown. Where a warm restart forms part of the approved procedure, check it separately from the initial start. A normal cold start does not automatically establish normal warmed-engine restarting.
STEP 06 — Post-Run Inspection
After the engine has stopped and all rotating components are stationary, inspect the engine mounting, control routing and cutting-side connections for visible movement, loosening or unintended contact.
4. Identify the Operating Stage Where a Fault Appears
A wheeled brush cutter combines an engine, mounted frame, operator controls and driven cutting assembly. An abnormal sound or vibration does not automatically identify which part is responsible.
The point at which the symptom appears is often more useful than a general description such as “unstable engine.” This allows a brush cutter manufacturer to investigate the appropriate assembly before making adjustments.
| Observed Condition | Inspection Priority | What Not to Assume |
| Engine struggles during initial operation. | Verify four-stroke preparation and starting-control operation before engine adjustment. | That the carburetor is necessarily defective. |
| Engine speed remains high after releasing the trigger. | Inspect throttle trigger, cable routing and return movement. | That carburetor adjustment is the first solution. |
| Engine accelerates, but cutting drive behaves irregularly. | Inspect the clutch, transmission and cutting-side assembly. | That engine acceleration and drive engagement are the same check. |
| Vibration becomes significant only after cutting engagement. | Inspect cutting attachment, driven components and relevant mounting points. | That vibration originates in the engine alone. |
| Entire machine shakes while engine speed appears stable. | Check frame, mounting hardware and structural connections. | That changing engine settings will correct loose structural components. |
These are diagnostic starting points, not automatic fault conclusions. If significant abnormal vibration, loose components or unsafe cutting-system behavior is observed, operation should stop until the cause has been assessed and corrected.
5. Do Not Turn 10000 RPM Into a Factory Acceptance Target
The TM-WBC435 lists 10000 rpm maximum speed and 1.1 kW rated output at 6500 rpm. These figures serve different technical purposes. A maximum-speed specification should not be interpreted as an instruction to operate each finished machine continuously at that speed during inspection.
The final production test should establish normal operation according to the approved procedure. Idle behavior, throttle return, cutting-system engagement and shutdown are individual checks; none becomes more informative simply because the engine has been pushed toward the largest number in the product specification.
Factory testing distinction
Correct: Confirm consistent operation at the relevant test stages under the approved procedure.
Incorrect: Treat the listed 10000 rpm maximum as the required operating target for every production unit.
This also matters when comparing factory inspection reports. A record that simply states “engine reached maximum speed” gives less information about finished-machine assembly than observations covering warm idle, control return, normal drive engagement and stop-switch function.
6. TM-WBC435: Product Reference for Finished-Machine Testing
The TM-WBC435 is relevant to this inspection method because its GX35 four-stroke engine and wheeled cutting structure require the factory to assess both engine operation and the response of the complete machine. It is a reference for grass-clearing equipment used in settings such as farms, gardens and roadside maintenance.
|
MODEL REFERENCE TM-WBC435GX35 Wheeled Brush Cutter
|
Engine: GX35, four-stroke, air-cooled Displacement: 35.8cc Rated output: 1.1 kW / 6500 rpm Idle speed: 3000 ±200 rpm Maximum speed: 10000 rpm Carburetor: Diaphragm type Fuel tank: 800 ml Net weight: 18.0 kg |
For procurement approval, the important question is not whether the TM-WBC435 suits every grass-clearing market. It is whether the production machines delivered under the confirmed specification operate consistently with the approved reference. Model selection and final manufacturing inspection should remain separate decisions.
7. Use Representative Batch Samples and a Final-Test Checklist
Routine production inspection and importer sampling have different roles. The factory should follow its normal production controls, while the importer or appointed inspector may select representative completed machines for additional verification under the agreed inspection plan.
One corrective adjustment on an individual unit may be a localized issue. If many finished machines require noticeably different adjustments to achieve normal operation, a common production or component cause deserves investigation. Repeatedly compensating for inconsistent assembly does not establish stable manufacturing control.
The following checklist focuses on evidence that can be collected from a TM-WBC435 finished-machine functional test without inventing test durations, inspection quantities or acceptance tolerances.
A short factory test is intended to identify final-assembly and operating inconsistencies. It should not be confused with a long-duration endurance test or with a market suitability evaluation for farms, gardens or roadside applications.
8. FAQ: GX35 Wheeled Brush Cutter Final Testing
Is starting the engine enough for a brush cutter manufacturer final test?
No. A successful start does not confirm stable warm idle, throttle return, cutting-system engagement, shutdown or post-run assembly condition. Each stage provides different information about the finished machine.
Why should the GX35 engine be checked after warm-up?
Starting controls and engine temperature can influence behavior immediately after a cold start. The TM-WBC435 idle reference of 3000 ±200 rpm is more useful when the engine has reached an appropriate operating condition and the throttle has been released.
Should every TM-WBC435 be tested at 10000 rpm?
The listed 10000 rpm is a maximum-speed reference, not an automatic continuous test target. Production testing should follow the applicable approved procedure rather than using the largest specification value as the main acceptance condition.
What causes abnormal vibration during a wheeled brush cutter test?
Possible inspection areas depend on when the vibration appears. Engine-side behavior and mounting should be considered if vibration occurs before cutting engagement. If it develops after engagement, the cutting attachment, transmission and related mounts become relevant. Loose frame components can also cause whole-machine movement.
Why is throttle return checked repeatedly?
One successful acceleration does not establish consistent control operation. Repeated acceleration and release can reveal sticking triggers, incorrect cable routing or inconsistent return movement that might otherwise be mistaken for a carburetor problem.
How should importers inspect GX35 wheeled brush cutters before a bulk shipment?
Use an agreed inspection plan and select representative completed machines for additional checks. Verify the GX35 identification, correct four-stroke preparation, starting behavior, warm idle, throttle response, cutting engagement, shutdown and post-run assembly condition. Any repeated abnormality should be investigated before shipment approval.
9. Confirm a Repeatable Final Test Before Bulk Shipment
The TM-WBC435 combines a GX35 four-stroke engine, 35.8cc displacement, 1.1 kW output at 6500 rpm and a wheeled machine structure. Those specifications identify the model, but a brush cutter manufacturer final test provides the practical operating evidence needed after assembly.
Before approving a bulk shipment, confirm the finished-machine configuration, the factory's applicable test sequence and how abnormalities will be recorded and corrected. The key result is consistent operating behavior across the selected production units, not simply evidence that the engines can start.
|
Review the TM-WBC435 for Your Next Order Use the model specification as the starting reference for discussing GX35 configuration, finished-machine inspection and bulk-order requirements. |
|
|